Introduction: Efficient Branching in Polyethylene Pipelines
In municipal water distribution, industrial raw water conveyance, and factory process manifolds, creating off-take branches from existing main pipelines is a regular engineering requirement. Cutting a main pipeline to insert an in-line reducing tee requires pipeline depressurization, extensive downtime, multiple butt-fusion or electrofusion welds, and substantial labor costs. Polypropylene (PP) and HDPE service saddles provide an engineered, cost-effective alternative for rapid branch tapping without cutting the main header.
Design Configurations: Mechanical Clamp Saddles vs. Electrofusion Saddles
1. Mechanical Clamp Saddles (PP / HDPE with SS Hardware)
Mechanical service saddles consist of two molded thermoplastic half-shells (upper body with threaded outlet boss, and lower back-strap clamp) fastened around the pipe perimeter with SS 304 or SS 316 bolts, nuts, and washers. An elastomeric O-ring or contoured profile gasket (NBR or EPDM) provides a compression seal against the outer pipe surface.
- Female BSP / NPT Threaded Outlets: Range from 1/2″ up to 3″ for quick connection to air release valves, pressure gauges, chemical dosing quills, or branch pipes.
- Reinforcing Metal Rings: High-performance saddles incorporate stainless steel reinforcement rings molded around the female threaded outlet to prevent radial stress cracking when metal nipples are tightened into polymer threads.
2. Electrofusion Branch Saddles
Electrofusion saddles feature an embedded heating element on the concave saddle base. The saddle is mechanically clamped to the scraped pipe and welded via an electrofusion processor. Once cooled, the integrated cutter (under-pressure drilling tool) cuts the pipe coupon internally while the main pipeline remains pressurized—a process known as hot tapping.
Step-by-Step Installation Protocol for Mechanical Saddles
- Surface Preparation: Thoroughly clean the outer pipe surface where the saddle will seat. Remove mud, oil, scale, and deep gouges.
- Gasket Seating: Verify that the O-ring gasket is firmly positioned in its molded groove without twisting or displacement. Apply silicone lubricant if recommended.
- Symmetrical Bolt Tightening: Fit the upper and lower halves around the pipe. Tighten diagonal bolts incrementally in an alternating sequence to ensure uniform gasket compression across the circumference. Avoid over-torquing that could deform thin-walled PE pipes.
- Tapping (Hole Drilling): Use a specialized shell hole-saw with a coupon-retaining pilot drill. Drill cleanly through the pipe wall without touching the internal saddle threads. Flush chips thoroughly prior to connecting downstream piping.
Engineering Considerations & Temperature Derating
When engineering branch connections on HDPE lines:
- Pressure Class Match: Ensure the saddle pressure class (e.g., PN 10 or PN 16) matches or exceeds the main pipeline working pressure.
- Thermal Derating: Polyethylene strength decreases with rising temperature. For pipelines operating above 20°C, apply standard ISO 4427 derating factors (e.g., 0.87 at 30°C, 0.74 at 40°C).
- Dynamic Vibration Isolation: If connecting heavy brass valves or motorized actuators to a saddle branch, provide independent pipe hanger supports so bending moments are not transferred directly to the saddle boss.
Comprehensive Piping Systems from Nikunj Fibreglass
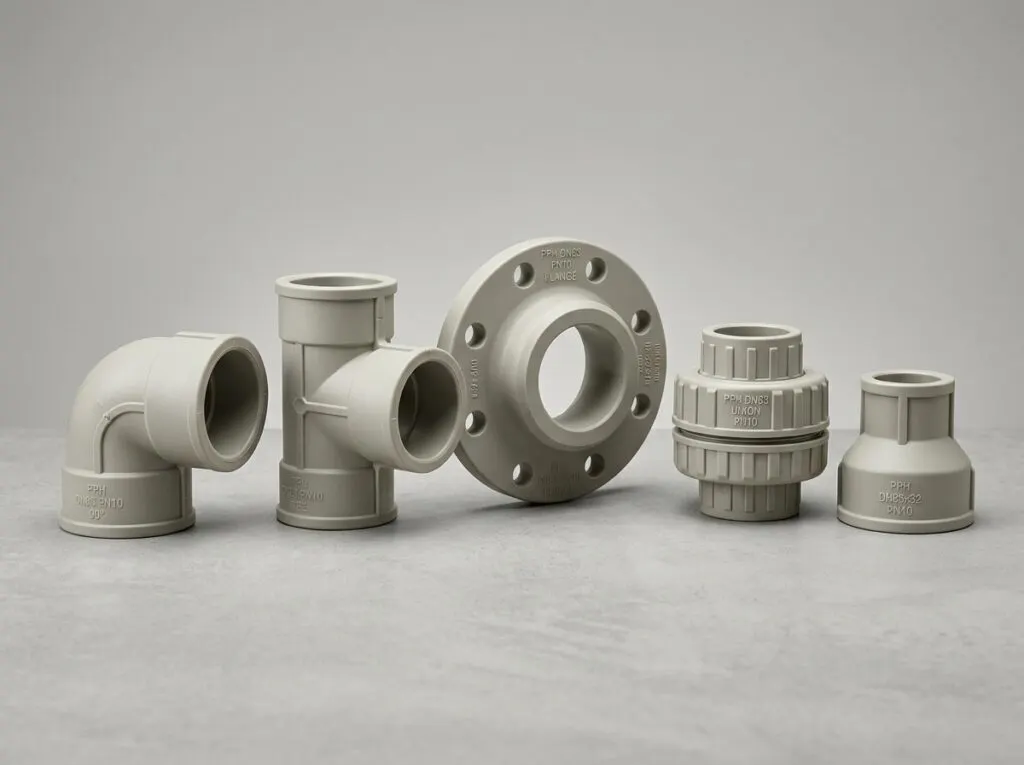
Alongside specialized saddles, Nikunj Fibreglass delivers a complete suite of industrial fluid conveyance solutions, including PP pipe fittings, industrial CPVC piping, and custom-fabricated FRP manifolds engineered to withstand India’s harshest industrial environments.